Home > Vibrators and unbalances > Foot mounted electric vibrators > MVSI-E > Vibrator motor MVSI-E
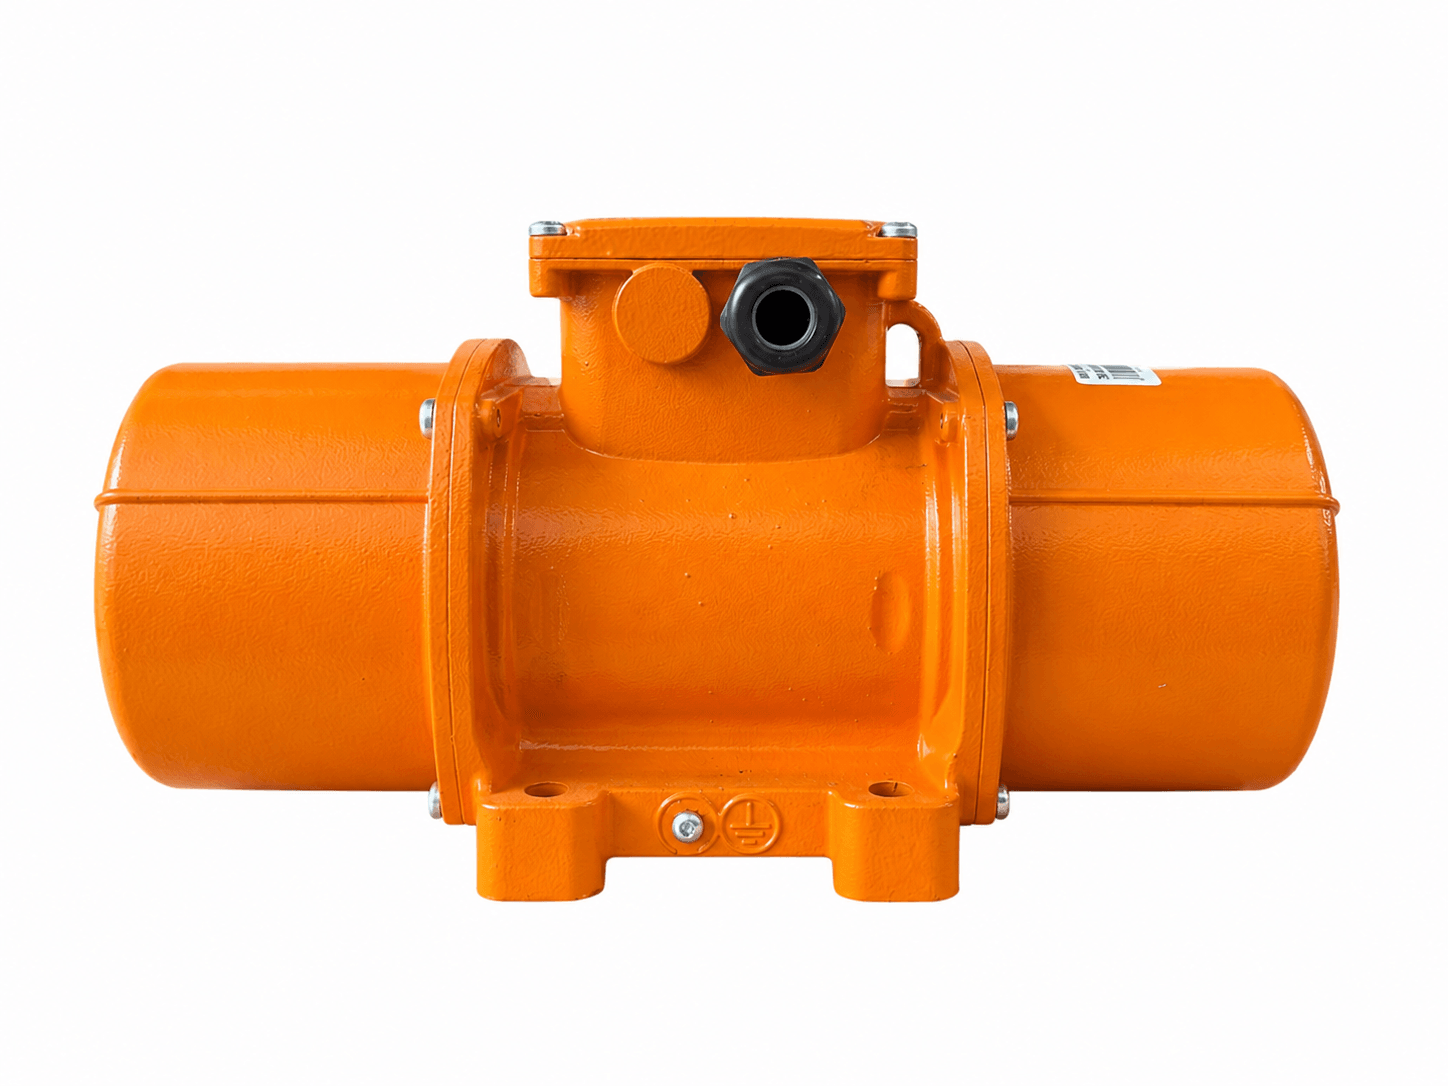
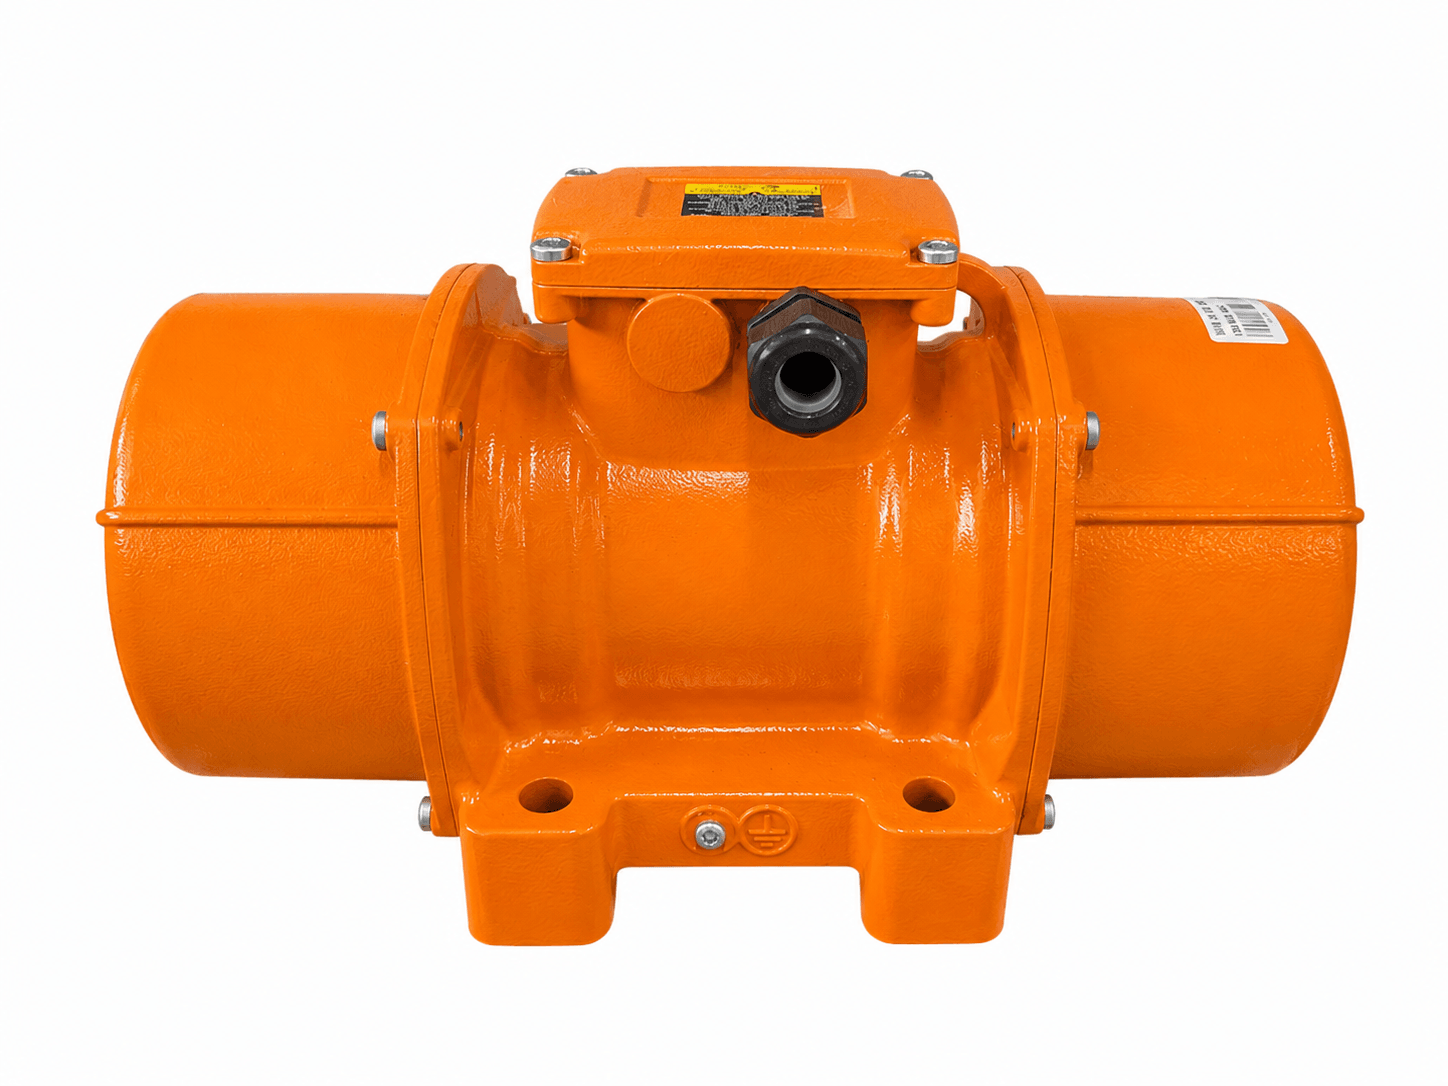
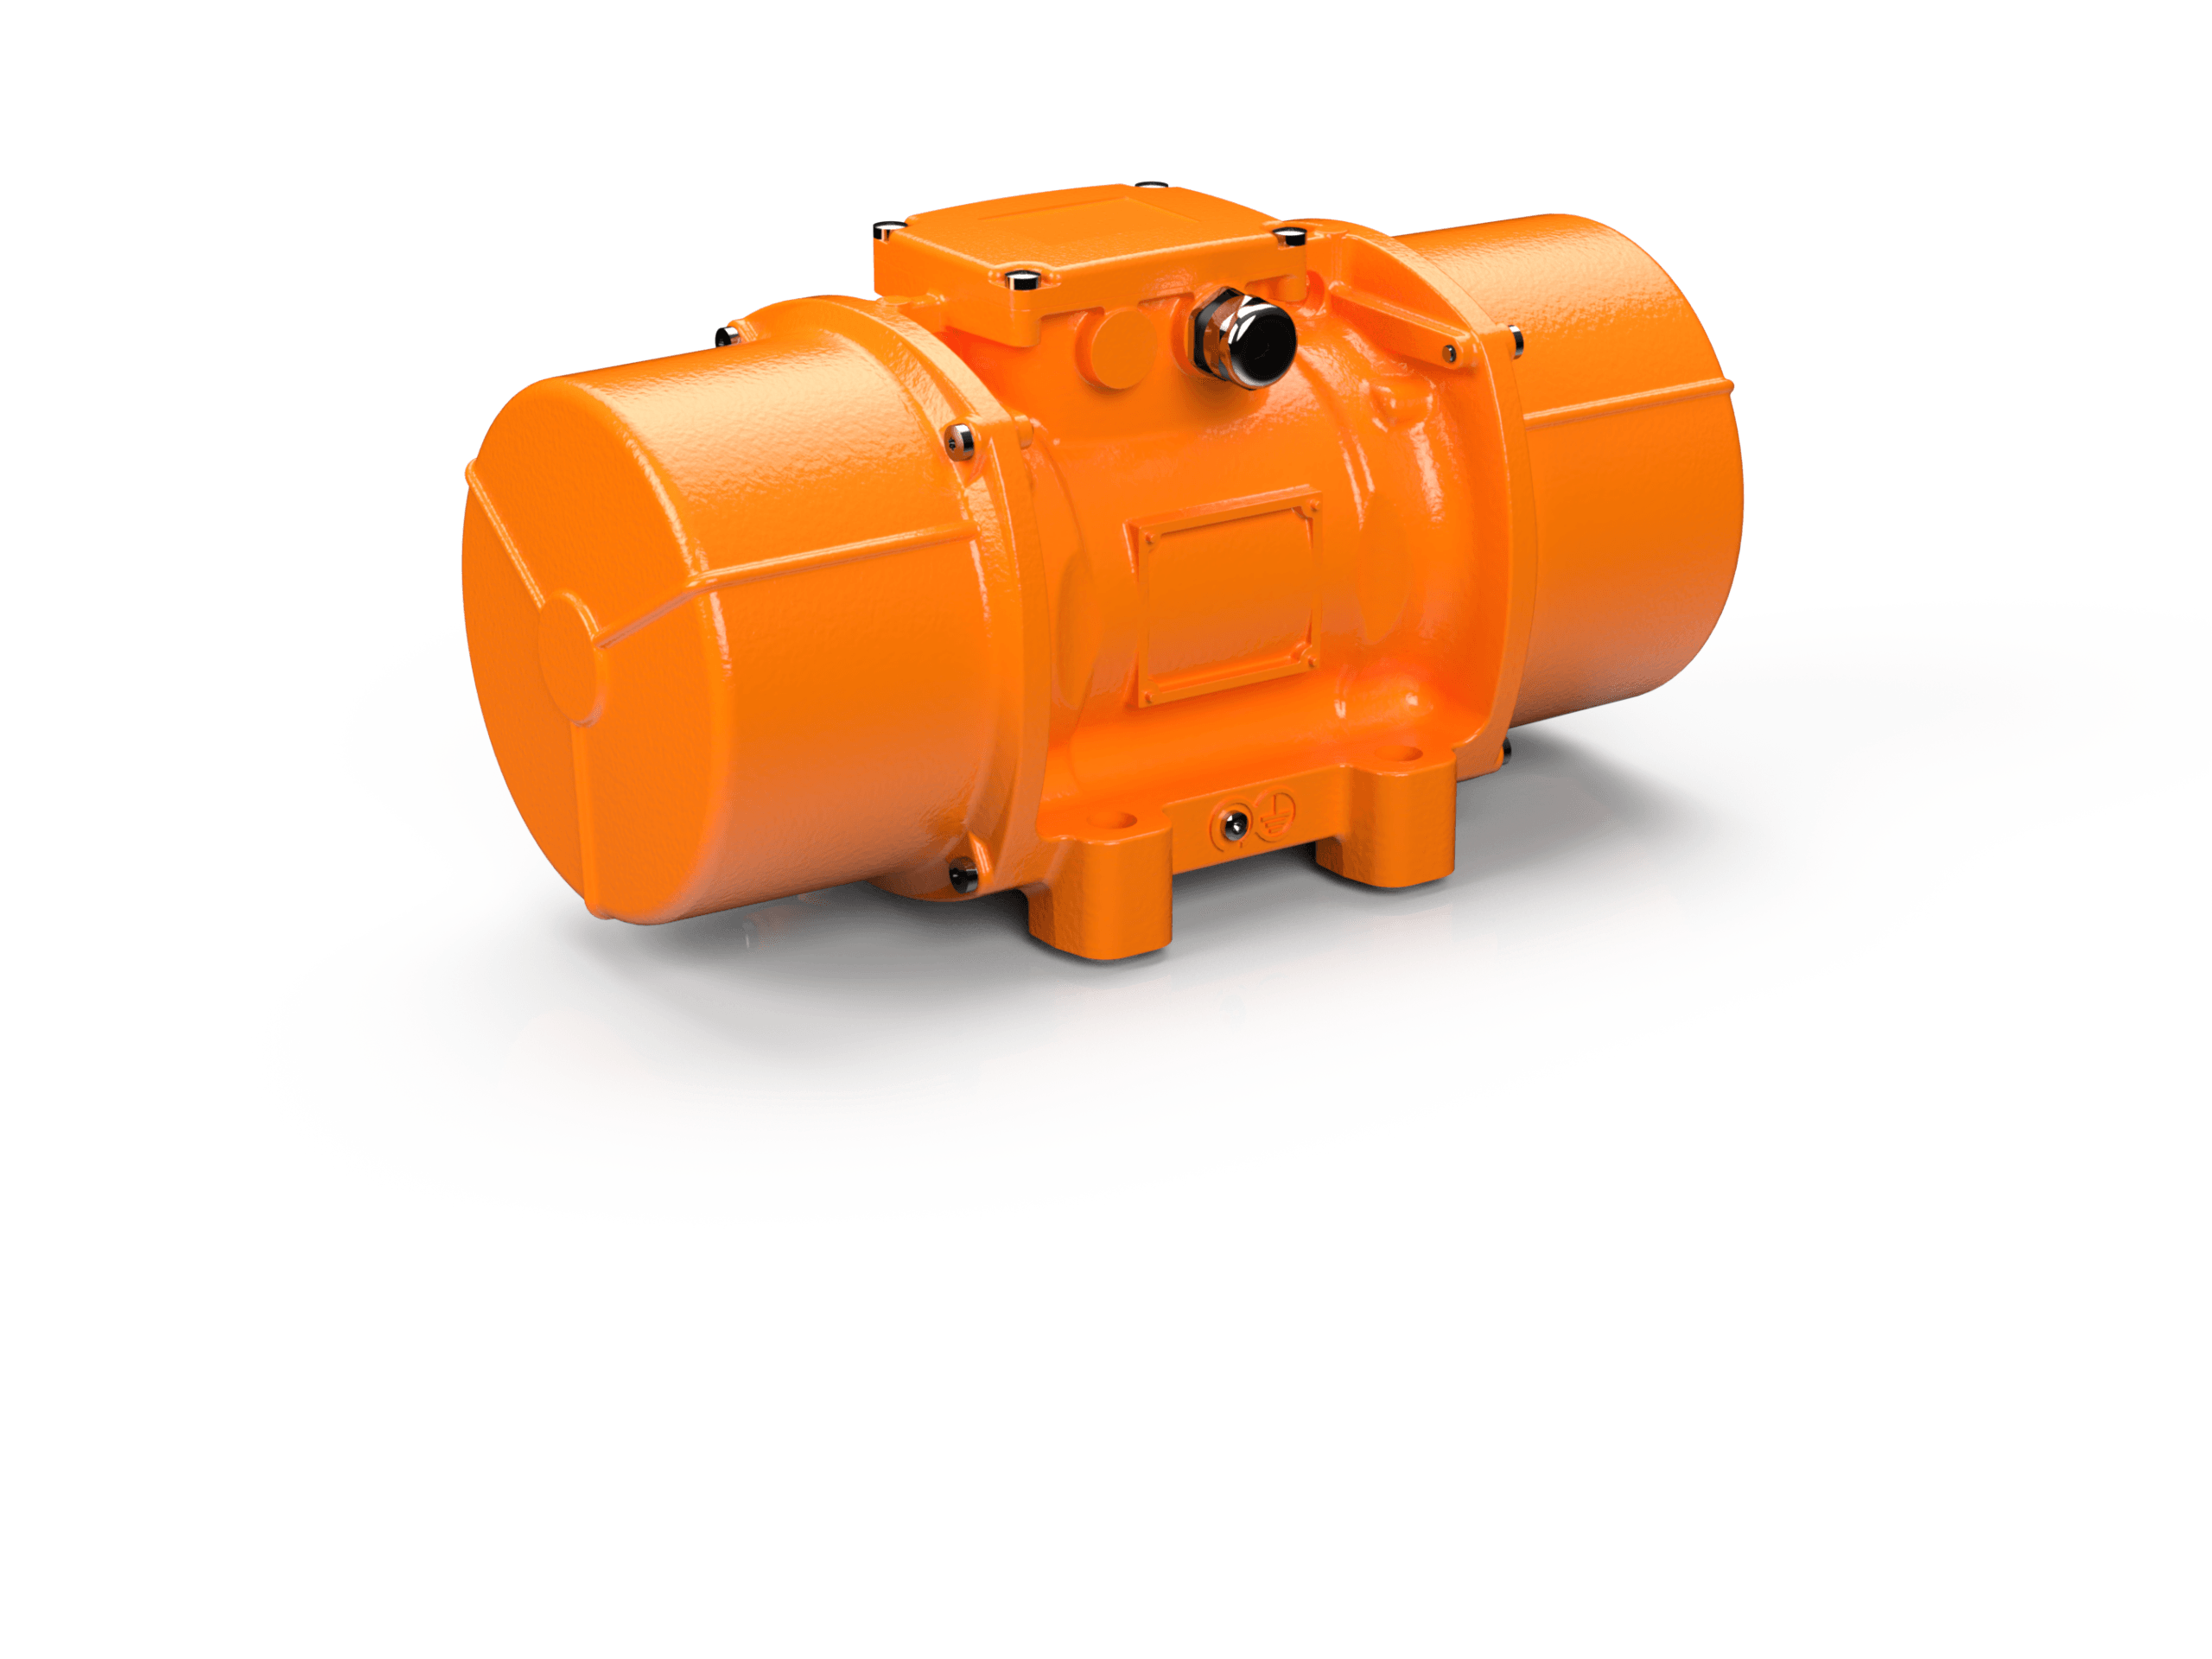
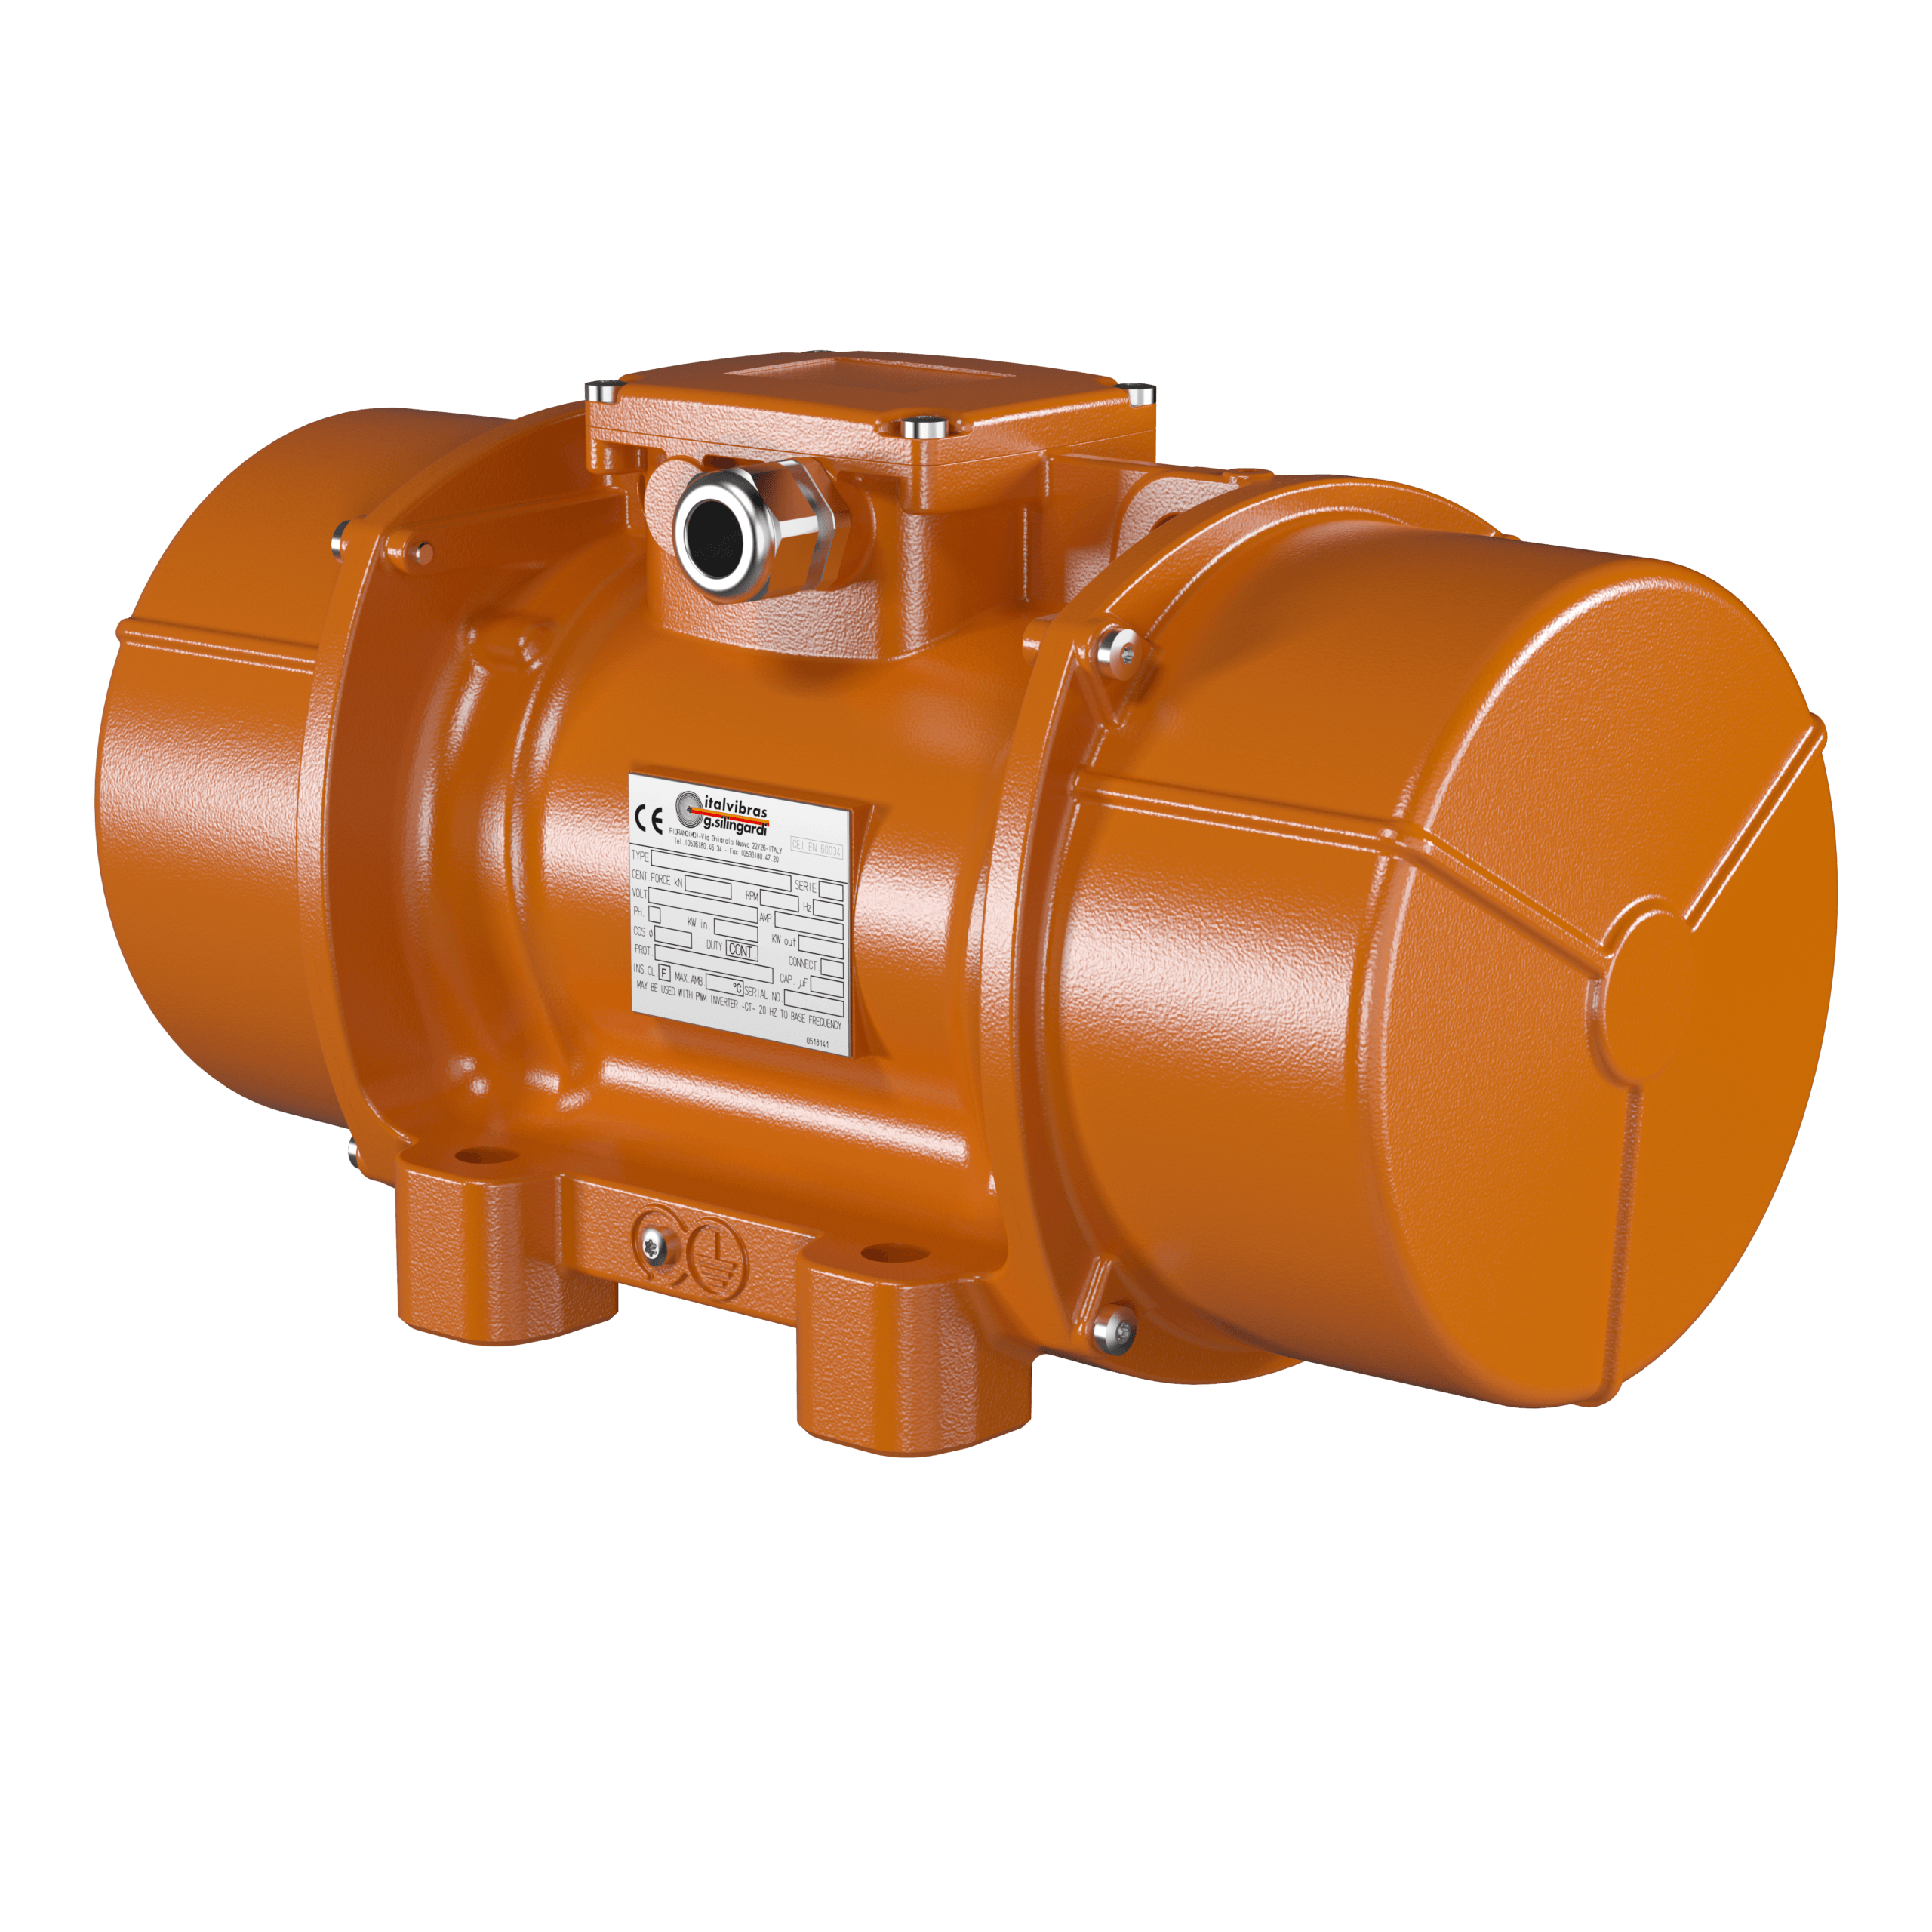
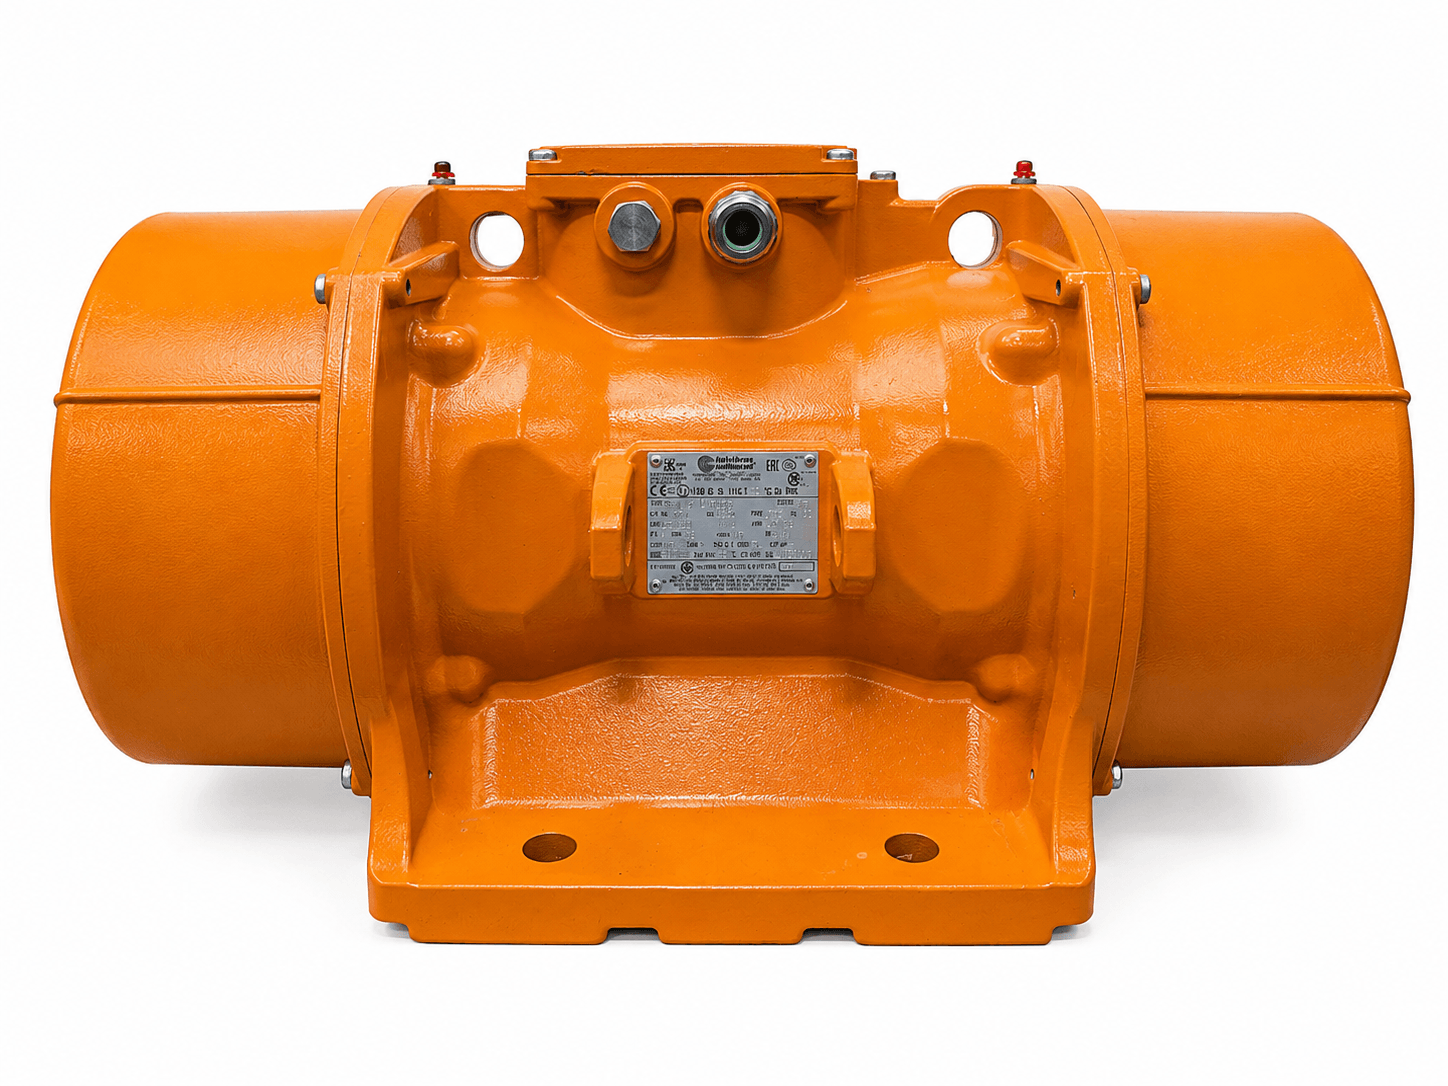
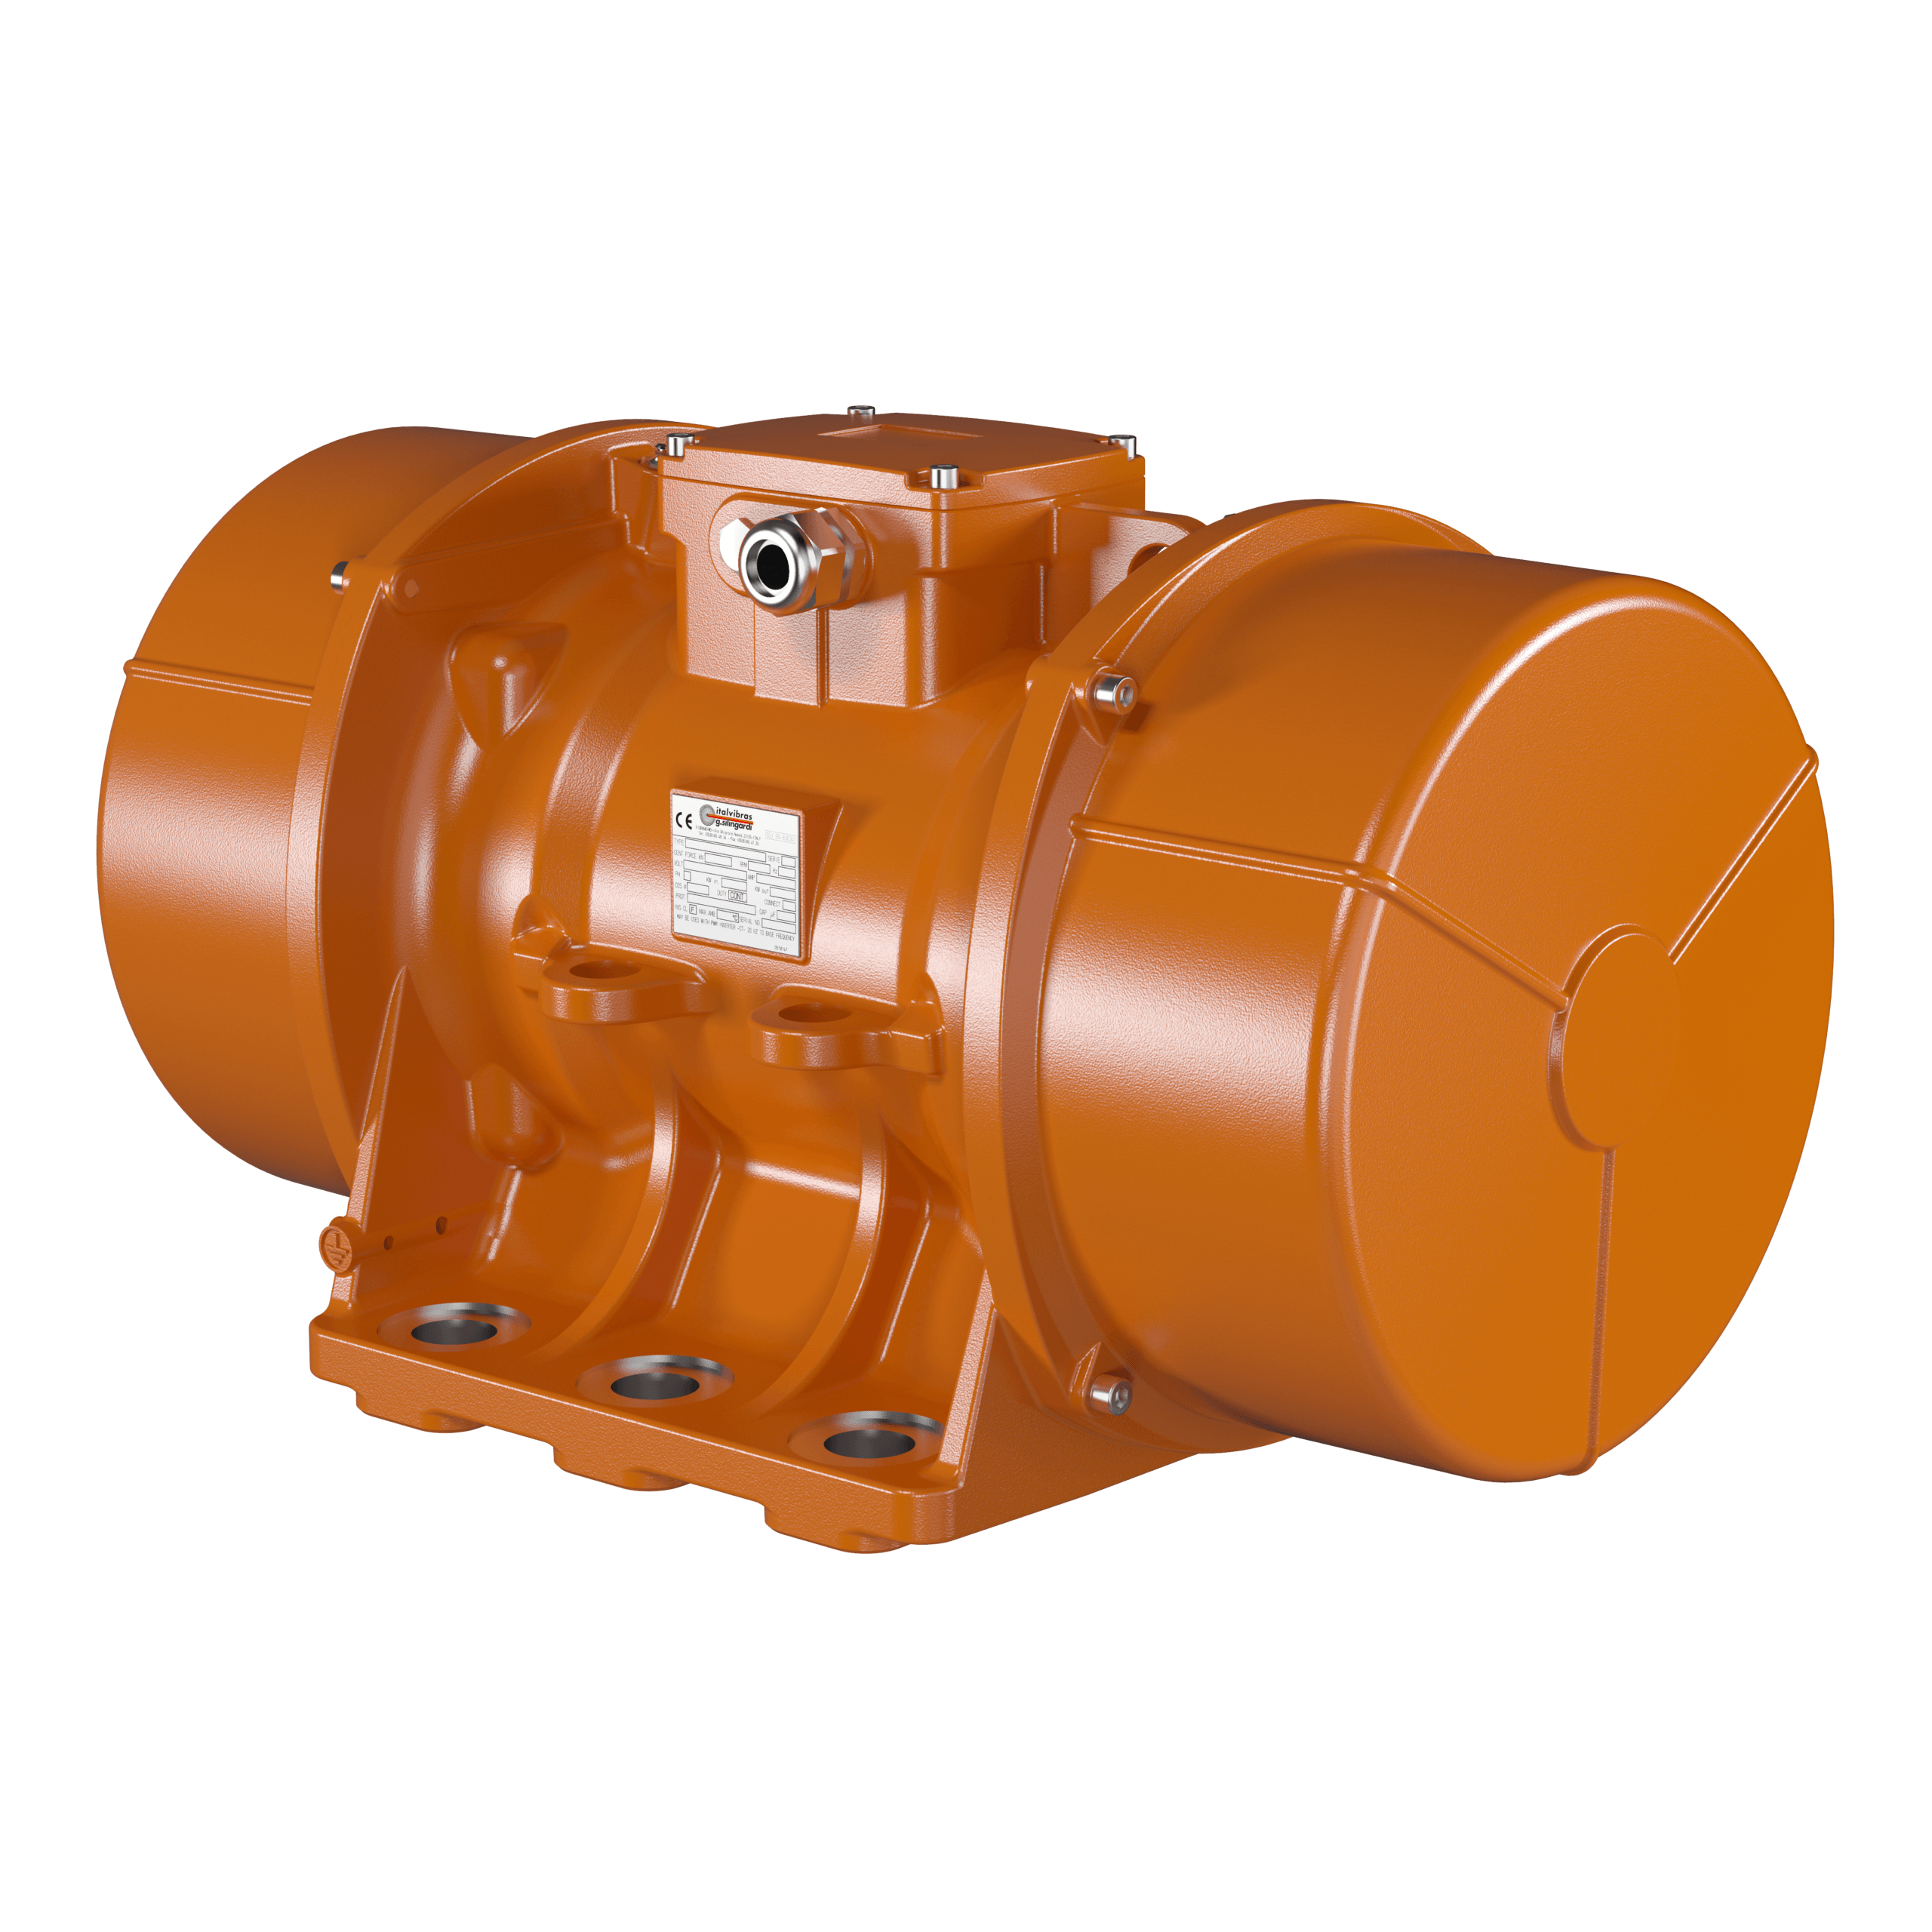
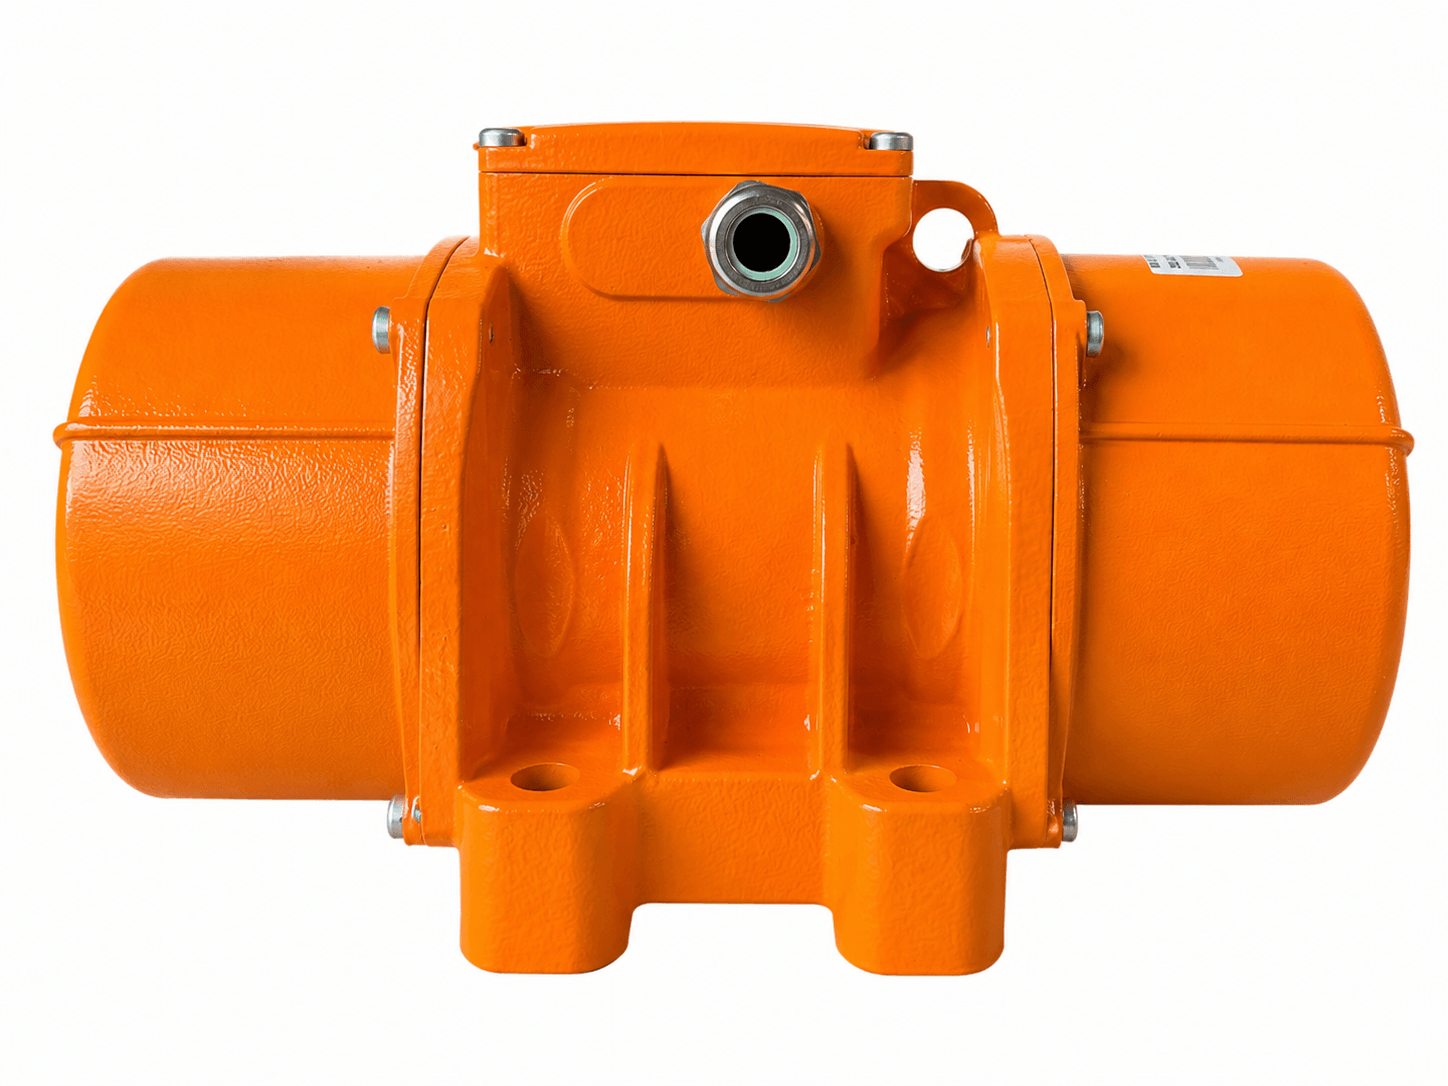
The MVSI-E range takes over the foot-mounted MVSI electric vibrator motors, with an ATEX certification that makes them usable in explosion-risk areas — both in the presence of gas (zones 1 and 2) and of combustible dust (zones 21 and 22). Available in 2, 4, 6 and 8 poles — the number of poles sets the speed, the figure after the « / » gives the centrifugal force (in 1/10 kg).
⚠ ATEX CERTIFIED II 2GD — GAS ZONES 1/2 & DUST ZONES 21/22Choose a polarity, then scroll the row horizontally : all these references are ATEX certified with increased safety.
Many short impulses : releasing, de-aerating, fine screening
The most common compromise : hoppers, silos, conveyors
Wider motion : wet, cohesive products, stubborn bridging
10/200E-S021,80 kN
10/310E-S023,15 kN
10/550E-S025,02 kN
10/810E-S087,94 kN
10/1110E-S0811,1 kN
10/1400E-S0814,0 kN
10/1610E-S0816,1 kN
10/2100E-S0821,1 kN
10/2610E-S0225,5 kN
10/3000E-S0229,5 kN
10/3810E-S0237,5 kN
10/4700E-S0246,1 kN
10/5200E-S0251,1 kN
10/5150E-S0251,3 kN
10/5700E-S0255,4 kN
10/6600E-S0266,7 kN
10/10000E-S0295,1 kN
10/11200E-S02contact us| Family | Speed | Centrifugal force | Why this choice |
|---|---|---|---|
| 3/XXXE — 2 poles | 3,000 rpm | 1,20 à 50,9 kN | Fast, fine vibration: screening, fluidising powders, small compact ATEX installations. |
| 15/XXXE — 4 poles | 1,500 rpm | 2,09 à 82,6 kN | A compromise between speed and amplitude: the default choice for most petrochemical and pharmaceutical installations in ATEX areas. |
| 10/XXXE — 6 poles | 1,000 rpm | 1,80 à 109 kN | Wider and slower vibration: hoppers and silos that are hard to empty, conveyors in hazardous areas. |
| 075/XXXE — 8 poles | 750 rpm | 1,02 à 76,4 kN | Very wide vibration at low frequency: large hoppers and silos, compaction, heavy structures in ATEX areas. |
A question about the reference or the temperature class suited to your installation? Contact our technical team.
The MVSI-E suits the same applications as the standard MVSI — hoppers and silos, conveyors and chutes, sieves and screens, compaction tables — but its ATEX certification makes it mandatory as soon as the installation is in an explosion-risk area. Four questions are enough to choose the right reference:
1. Gas area or dust area? The MVSI-E is certified II 2GD, so valid for both: zones 1 and 2 (gas) and zones 21 and 22 (combustible dust). A single vibrator motor covers both types of risk if your installation combines them.
2. Which temperature class, T3 or T4? Class T3 allows a higher surface temperature and therefore a higher power; the stricter class T4 imposes a reduced power. The choice depends on the auto-ignition temperature of the gas or dust present — to be confirmed with your design office before ordering, as this parameter cannot be changed afterwards.
3. What centrifugal force is needed? As for a standard MVSI, it depends on the weight of the structure to be vibrated and on the nature of the material. A common sizing rule for a hopper: the centrifugal force required is usually between 1/20 and 1/10 of the weight of material held in the conical section.
4. What speed suits? A 2- or 4-pole gives a fast, fine vibration; a 6- or 8-pole gives a wide, slow vibration, better suited to large structures or materials that are hard to release, with less wear on an installation running continuously.
For installation, electrical connection and maintenance in ATEX areas, see our full guide to the Series E vibrator motors, with detailed technical drawings.
If in doubt, our technical team can help you size the exact reference from your application — get in touch.
Neighbouring families and useful resources to refine your choice.